Exhaust Manifold Torque Sequence for DIY Installers
Start exhaust manifold bolts at the center, then move outward in an alternating pattern, tightening in about 2–3 torque stages to the factory spec. Skip that order, and you can warp the manifold, crush a gasket unevenly, or strip a head thread, turning a small leak into a broken fastener. This guide covers the correct tightening pattern, stage-by-stage tightening, and the checks that tell you when torque alone will not seal a warped flange, damaged thread, or mismatched gasket.
What you’ll need


- OEM service manual torque specification for the exact engine
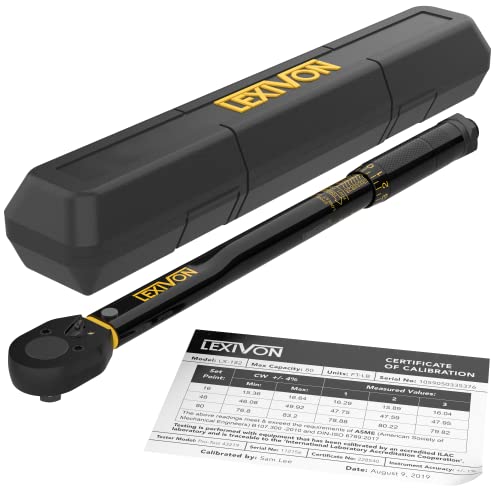
- Torque wrench that covers the required range; a low-range inch-pound wrench is often needed for small fasteners
- Correct socket for the bolt head or nut, plus a short extension if access is tight
- New exhaust manifold gasket that matches port shape, bolt pattern, and thickness
- Brake cleaner or equivalent non-residue cleaner for mating surfaces
- Straightedge and feeler gauge for checking flange flatness
- Thread chaser or tap of the correct size, if threads need cleanup
- Thread inserts, studs, or replacement hardware if the OEM repair path calls for them
- Approved thread sealant or anti-seize only if the service manual allows it
How do you tighten an exhaust manifold?
Use the OEM sequence, start at the center, and tighten in stages until the final pass reaches spec. The center-out pattern helps keep the flange flat, while staged tightening lets the gasket compress evenly and keeps one bolt from pulling the manifold crooked before the rest of the fasteners load.
-
Verify the exact spec.
Check the service manual for the engine code, bolt size, and fastener grade, then note the torque value and whether the final figure is in inch-pounds or foot-pounds. Do not mix specs from similar engines; thread size and head material change the safe clamp load.
-
Clean and inspect parts.
Clean the head face, manifold flange, and bolt holes with a non-residue solvent. Check for stripped aluminum threads, broken studs, pitting, carbon tracks, and gasket material left behind, because torque cannot make up for damaged contact surfaces.
-
Fit the gasket correctly.
Install a new gasket if the old one is crushed, torn, or heat-damaged. Its port shape, bolt pattern, and thickness must match the manifold and head exactly; reuse only if the OEM explicitly allows it and the part is still within spec.
-
Snug the fasteners evenly.
Run all bolts or nuts down by hand first, then snug them just enough to seat the manifold without forcing it. If a fastener binds early, stop and correct the thread; forcing it can cross-thread the head or snap a stud.
-
Tighten in stages.
Use 2–3 passes. A common approach is about 30%, then 60%, then 100% of final torque, following the manual’s order each time. Staging matters because some gaskets compress more on the first pass than others.
-
Recheck the final pass.
Make the last pass with a calibrated click or digital torque wrench. If the wrench never clicks on a fastener that should be moving, stop and inspect for thread damage, a warped flange, or a gasket that is not seating flat.
Exhaust manifold tightening decision table
This table gives a center-out decision rule when the manual is silent or when you need a layout-specific order. If the OEM specifies a different sequence, follow that instead. Use the stop conditions to decide when more torque will only create damage.
| Layout | Recommended bolt order | Staged passes | Stop condition |
|---|---|---|---|
| Inline 4-cylinder | Center pair, then move one fastener outward on each side in alternating left-right order | 3 passes: 30%, 60%, final spec | Stop if one corner lifts, the flange rocks, or a bolt bottoms before clamp load builds |
| Inline 6-cylinder | Middle fasteners first, then alternate outward toward both ends | 3 passes: light seat, mid-pass, final spec | Stop if the middle seals but the ends gap, which points to warp rather than loose torque |
| V-engine bank manifold | Start at the center section of that bank, then alternate front and rear fasteners outward | 2–3 passes depending on gasket thickness | Stop if access is poor enough that the wrench cannot sit square on the fastener |
| Split manifold or divided port design | Tighten each section from its center outward, then cross-check both sections for even load | 3 passes, with a pause after the mid-pass | Stop if one section seals and the other still ticks after the final pass |
| No OEM order available | Use the center-out alternating pattern that keeps the flange flat | 3 passes, with the final pass at the listed torque only | Stop for stripped threads, broken studs, missing gasket match, or visible flange warp |
Can torque sequence fix a leak?
No. Sequence can help a sound part seal, but it cannot repair a warped flange, damaged threads, or a gasket that does not match the ports. If the manifold or head surface is out of flat, more torque often makes the leak worse by bending the flange harder into the high spots.
Say your inline-four ticks at cold start, and one end of the manifold still shows soot after the final pass. That pattern often points to a flange that is bowed near the end bolt or a gasket that is too thick for the ports, not a simple loose-fastener problem.
Warped flange checks
Lay a straightedge across the flange in several directions and check the gap with a feeler gauge. If the surface is out of spec, resurfacing or replacement is usually the practical fix. Tightening harder may only squeeze the gasket at the corners and leave the center leaking.
- Measure flatness. Check lengthwise, across the ports, and diagonally.
- Compare to spec. Use the service manual’s flatness limit, if listed.
- Stop on out-of-spec warp. Resurface or replace instead of increasing torque.
Stripped aluminum threads
Aluminum heads are less forgiving than cast iron heads. If a bolt spins, pulls up too easily, or never reaches spec, the threads may be stripped. Install the correct thread insert or repair hardware before attempting final torque, because a weak thread can let a fastener loosen after heat cycling.
- Test each hole. Thread the bolt in by hand first.
- Repair damaged threads. Use the OEM-approved insert size and depth.
- Recheck torque. Restart the staged tightening only after the repair holds.
Gasket mismatch and thickness problems
Gasket thickness changes clamp load, and the wrong port shape can leave one runner half-covered. A multi-layer steel gasket and a graphite gasket do not behave the same under load. If the gasket does not match the manifold pattern, replace it rather than trying to crush it into place.
- Confirm the part number. Match engine code and manifold layout.
- Inspect the imprint. Uneven compression means the gasket is wrong or the flange is distorted.
- Replace mismatched parts. Do not add extra torque to cover a fit problem.
Common mistakes
- Using one torque value for every engine. Bolt size, grade, and head material change the correct spec.
- Skipping the center-out order. This can bow the manifold before the outer bolts seat.
- Torquing in one pass. A gasket that compresses unevenly can leave a corner loose even when the wrench hits spec.
- Applying anti-seize without approval. It lowers friction and can raise clamp load at the same wrench reading, which may over-stress the fastener.
- Reusing a damaged gasket. A crushed or burnt gasket will not seal reliably, even with perfect torque sequence.
- Ignoring broken studs or spun threads. Torque sequence cannot fix missing clamp force.
Picture a V6 bank with one broken stud near the rear port. The remaining bolts may still reach spec, but the flange can still leak because the missing fastener leaves one area under-clamped. The repair order is stud replacement first, torque sequence second.
Frequently asked questions
What is the correct exhaust manifold torque sequence?
The correct sequence is the OEM order when one is listed. If no order is provided, start at the center of the manifold and alternate outward toward both ends. That pattern limits flange bending and helps the gasket load evenly across the ports.
Do I torque exhaust manifold bolts from the center out?
Yes, that is the usual default for most layouts. Center-out tightening reduces the chance of drawing one end down first and warping the flange. Inline engines usually alternate outward from the middle; V engines often follow the center section of each bank outward.
Should I torque exhaust manifold bolts in stages?
Yes. Two or three stages are the normal approach, especially with thicker gaskets or long manifolds. A common sequence is a light seating pass, a mid-pass, and then the final torque value. Staging helps the gasket compress more evenly and lowers the risk of a crooked clamp load.
Do I need a new gasket before installing an exhaust manifold?
Usually, yes. Use a new gasket unless the OEM explicitly allows reuse and the old gasket is still undamaged. The port shape, bolt pattern, and thickness should match the manifold and head as closely as required by the fitment. A crushed or heat-baked gasket can leak even when the fasteners are torqued correctly.
What happens if exhaust manifold bolts are overtorqued?
Overtorque can stretch or snap the bolt, strip threads in an aluminum head, or warp the manifold flange enough to create a leak. It can also crush the gasket unevenly, which may seal one runner while opening another. If the wrench reading seems to “fix” a leak, inspect for damage instead of tightening farther.
Should I retorque exhaust manifold bolts after heat cycling?
Only if the service manual calls for it. Some engines allow a recheck after the first heat cycle, but torque-to-yield fasteners usually should not be retorqued. Wait until the engine has cooled fully, then inspect for leaks with the engine idling and again after a short road test.
Do aluminum heads need a different torque sequence than cast iron heads?
The sequence usually stays the same, but the risk level changes. Aluminum threads are easier to damage and may need inserts if stripped, while cast iron tolerates thread load differently. The torque value may also differ by head material and fastener type, so the manual matters more than the metal alone.
How do I tighten a warped exhaust manifold without causing leaks?
You usually do not. If the flange is out of flat, more torque can make the leak worse by flexing the manifold. Check flatness with a straightedge, then resurface or replace the part if it is out of spec. Tightening harder is not a repair for warp.
What torque wrench and socket size do I need for exhaust manifold bolts?
Use a calibrated torque wrench that covers the required range, often in inch-pounds for smaller fasteners and foot-pounds for larger ones. The socket size depends on the engine, but 10 mm, 12 mm, 13 mm, and 14 mm are common. Match the wrench range to the spec so the final click is accurate.